Page created on 07/04/2025; updated on 15/08/2026.
Preamble
Following my (predictable) disappointment with the Chinese mini-lathe, I ordered the Proxxon FD 150/E lathe, along with the essential accessories, sliding tailstock key chuck, and ER11 collet set.
I had already bought a set of cutting tools for the Chinese mini-lathe.

Presentation
Scope of contents
The lathe is delivered in its Proxxon packaging, with no discreet over-wrapping, increasing the risk of theft! Inside, the expanded polystyrene cushioning was inadequate and worn away; the accessories were not cushioned at all and were wandering around in the box. From this point of view, the Chinese lathe was better protected, and in a more environmentally-friendly way.

Here is a general view of the lathe as it comes out of its packaging, before the cranks are fitted.

In front of the lathe itself, you can see a bag containing the cranks, the spindle key and a case containing the movable tip and the chuck clamping levers.
First glance
Opening the protective cover, locked with a knurled screw, reveals the double V-belt drive, shown here in the high-speed position. The drive pulley is made of wood! Why not!

The belt is very taut: the tensioner is useless in this position, but useful in the low-speed position. On the inside of the cover, you can see the table showing the choice of speeds according to the material and diameter of the workpiece. The problem is that it is printed on a mirror background, which makes it difficult to read in certain conditions. Why not just white?
Start-up and shut-down are by push-button and self-holding relay, avoiding the risk of accidental restart after the mains voltage has been removed and restored. The three-pole 230 V power cable is 1.70 m long. I would have liked it to be disconnectable for easier storage. I am afraid the cable outlet will not last long.
The multilingual instructions are fairly detailed, although there are a few rough translations.
The whole thing weighs 4.5 kg, almost the same as the Chinese lathe.
Owner’s tour
The one-piece aluminium bed is fairly rigid (cross-section: 70 × 50). The tool carriage and chuck are made of steel. The tailstock and carriage each have a quick-release lever.
Clearances: the slides are well adjusted; only the cranks have some free play, which is unavoidable with the triangular threaded screws (M6 × 1). The gibs are made of brass.
The spindle shaft is hollow, allowing cylindrical bars with a maximum diameter of 8.5 mm to pass through.
Tool holder
The tool holder is also made of steel. It has two slots for 6 × 6 mm cutting tools, with a maximum height of 8 mm. The height of the cutting edge, for Proxxon tools ref. 24524, may require the addition of a spacer of up to 0.5 mm.
Spindle chuck
This steel chuck has three concentric jaws. Like the Chinese lathe, it is clamped by two lever-operated rods. This system is not very practical as it generally requires both hands, thus preventing the workpiece from being held at the same time.
Caution: the jaws have sharp, angular parts that can cause injury. The guard must therefore always be lowered when the chuck is rotating. However, when using when using ER11 collets with short workpieces, the guard practically prevents calliper measurements. It is better to remove it in this case.
There is another risk of injury that the guard will not protect against: this occurs when handling the dismantled chuck. The rear of the jaws has knife-shaped cams, which are rather sharp. I cut my thumb quite deeply this way.
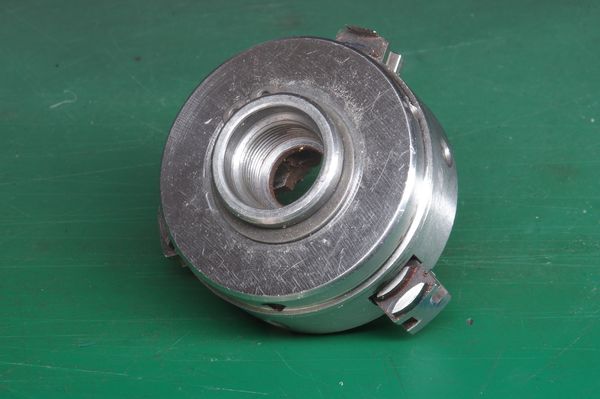
Click on the image to see the cam closer.
The chuck is secured by an M16 × 1 thread. Warning: when you mount the chuck on the spindle, using the spindle key and one of the two rods mentioned above, after screwing, you will feel a strong resistance which may lead you to believe that the tightening is complete. It’s nothing of the sort: it’s just the ⌀ 18 spindle shaft coming into contact with the chuck bore. You must therefore continue to clamp to overcome this resistance, until the final clamping occurs.
Tailstock
The aluminium sliding tailstock has a shaft with a tapered bore (this is not a Morse taper, as far as I can tell). A 10 mm diameter sliding tip is supplied. To disengage the cone, all you have to do is crank the tip back until it stops.
Tailstock chuck
This accessory is not supplied as standard. It has the same tapered shank as the movable tip, which guarantees concentricity.
ER11 collets
ER11 collets are also not supplied as standard. The diameters are: 2.0 - 2.5 - 3.0 - 4.0 - 5.0 - 6.0 and 7.0 mm. To use them, first fit the chosen clamp into the nut: it clicks into place. Only then is the whole assembly screwed to the spindle in place of the chuck.
Here are the tailstock chuck and ER11 collets.

Lathe accuracy
Chuck runout
The measurement is made using a dial indicator on a 5 mm nickel-plated brass rod. The magnetic base is fixed to the tool carriage, duly clamped, of course.

Here are the dial indicator readings in the extreme positions.
There is almost a 3/10 runout… Twice as much as on the Chinese mini-tour! I think this is a lot. Is there any way of acting on the jaws to reduce this defect? That remains to be seen.

Click on the image to see
the other dial indicator position.
Since then, I’ve taken measurements again, telling myself that you have to use ground bars to get reliable results. I chose drills of different diameters, from 6 to 10 mm, and found that the results vary for the same sample depending on its angular position in the chuck! For example, for a ⌀ 9 drill, I obtained values ranging from 3/100 (fantastic!) to 30/100 — ten times more!
Conclusion: I cannot conclude anything! When I want to obtain precision, I will have to make several attempts with the dial indicator to find the best position.
Aligning the chuck with the moving point
Alignment is difficult to measure. I will settle for a visual inspection to start with, complicated by the runout I noted earlier.

Click on the image for a closer look at the misalignment.
This misalignment is still very moderate. In fact, to judge the alignment properly, you would have to turn a fairly long workpiece with the moving tip, then accurately measure the diameters obtained at each end. They should ideally be equal. That said, as there is no adjustment on the sliding tailstock, I cannot see how to correct the misalignment.
Runout of ER11 collets
The measurement is carried out under the same conditions as with the chuck.

Here are the dial indicator readings in the extreme positions.
Here we have less than 4/100 runout, which I think is quite acceptable for such a modest lathe.

Click on the image to see
the other dial indicator position.
Alignment

Click on the image for a closer look at the offset.
This is not perfect, but as I said, it cannot be adjusted. Note that the movable tip moves — albeit very slightly — as the tailstock is clamped to the bed…
A few machining operations to learn the ropes
Turning a brass screw
I have a small stock of brass wood screws inherited from my father. The first test will be a TF 4 × 40 screw. After sawing off its head, I install it in the ER collet, not without noticing that the nonthreaded body is not cylindrical, but slightly conical: D1 = 4.0 at the head, D2 = 3.8 at the start of the thread.
Turning consists of removing the thread to obtain a smooth part with a diameter of 2 mm. The part has obviously flexed, as the diameter is not constant along its length. The surface finish is not great,
Turning a brass screw (bis)
Same operation as above, but this time I first cut the tip of the screw and hollow out a centre with a PCB conical cutter. This one is not very rigid; I will have to buy a centring drill.

The turning is carried out with the centre point. It allows a greater depth of cut and the result is much better. One small drawback: the tailstock makes machining the end tricky. I obtained a diameter of 2.05 mm. First pass:

Result after finishing pass. In the foreground, an untreated guinea pig:

Turning a conductive ring
This is a ring to replace the insulation on the axle of an Express Nord LS Models coach. I remind you that, in order to increase the number of electrical contact points for the current pickup, I “short-circuited” the axle insulation ring with conductive paint. For other coaches, I had used brass tubes fitted one inside the other, but with a lack of tightening that led to the wheel buckling.
So here I am trying to make a ring in the same shape as the original insulating ring. Here are the dimensions.
From a ⌀ 6 brass rod, turning to the diameter of the collar (5.4 mm) over a distance of approximately 5 mm.

Turning to the outer diameter of the ring; I obtained 4.14. A little too small and there is no clamping in the wheel. Missed the mark? Not quite, we are about to see!

Boring the shaft. Here, I have no choice: 1.9 is really too small, 2.0 is a little too large — let us not forget that, because of the misalignment, the diameter obtained will be slightly greater than that of the drill — but, thanks to the splines on the spindle, there will be no floating.

To finish, I make a groove for cutting to length 4 mm.

A slight chamfer is made wherever necessary.
The ring is sawn using a bocfil, progressively, turning the chuck by hand to avoid any deviation. The rotating point is put in place to avoid losing the part once it has been separated from its support.

As the outside diameter is a little too small, and the bore a little too narrow (the splines, still…), the ring is split with a bocfil saw, so as to distribute the clamping over the two diameters.

The ring fitted showed no visible warping. The result is therefore satisfactory, but the process is long, very long!

Click on the image for a closer look at the ring.
Turning Märklin wheels
The aim is the same as for the conductive ring seen above: to obtain wheels not isolated from their half-axle. Nothing could be simpler than to use Märklin wheels. The problem is that they do not meet the NEM 310 standard: they are too wide (3 mm instead of 2.8) and have a huge flange (1.5 mm).
So I am going to machine them to get the correct width and a 0.8 mm flange. As their rolling diameter is 10.4 mm, the total diameter targeted will be 10.4 + 2 × 0.8 = 12.0 mm.
I need a prepared spindle to rotate the wheel during turning. I have chosen a steel axle (there are brass ones, not suitable here), which I have threaded about 7 mm. The smooth part will be taken in the ER11 collet.
Manual threading of the axle.
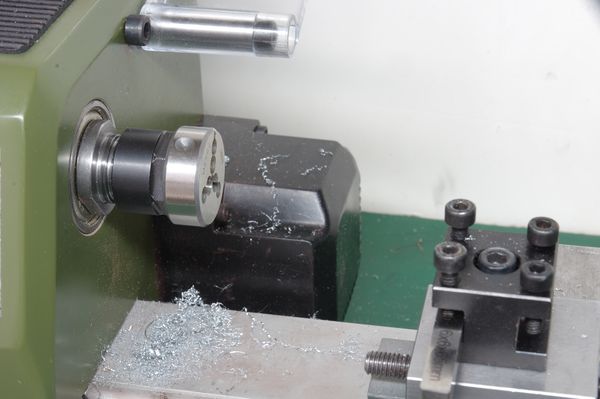
Here is the threaded axle.
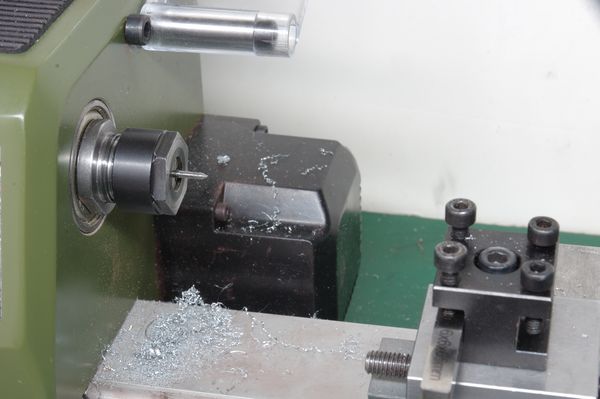
Click on the image for a closer look at the axle.
Fitting the wheel between two nuts with washers.
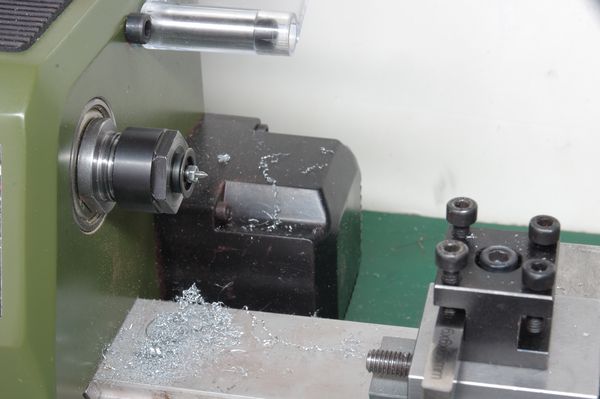
Click on the image for a closer look.
Cutting the diameter with the cut-off tool.

Click on the image for a closer look.
Cutting the width, using the carriage tool. On reflection, rather than removing the 0.2 mm on the inside flank, I should have done better to remove 0.1 mm on each side, as the resulting flange is a little too thin.
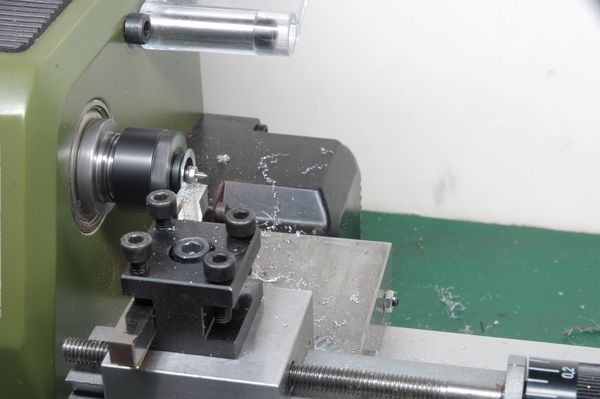
Click on the image for a closer look.
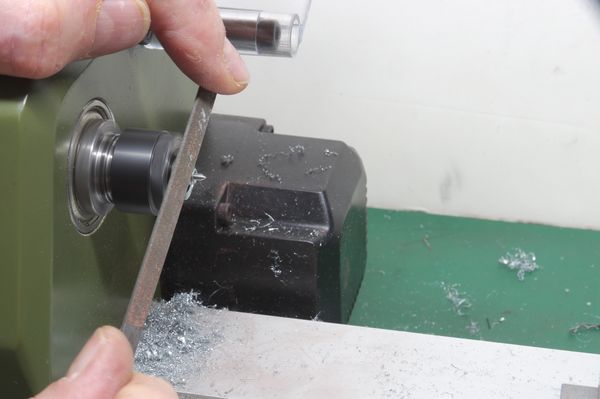
Rounding the flange with a file.
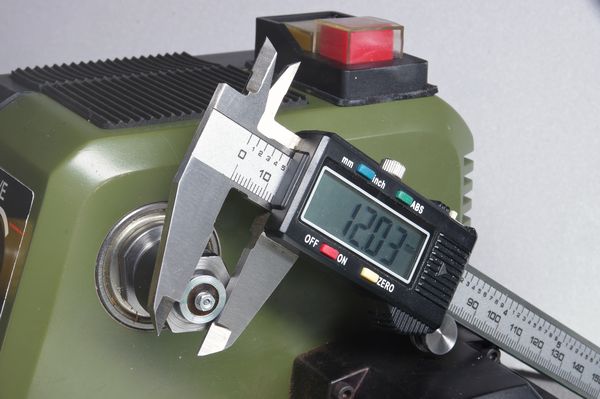
Checking the outside diameter. The values obtained range from 11.9 to 12.1. On the same wheel, the diameter varies by a maximum of 5/100 mm.
Notes:
- To make the measurement, I had to remove the guard, as mentioned above.
- In reality, I carry out each operation (reducing the diameter and then the width) in series for all the wheels I treat, to avoid changing tools and taking the origin from the wheel over and over again.
Improving the process
For a second series of wheels, I improved the process:
- The wheel to be machined is no longer supported by the thread, but by the smooth part of the axle, which virtually cancels out the radial play, sometimes at the cost of a risk of jamming. As a result, there is no longer a nut behind the wheel; it rests directly on the collet nut, which is beneficial for orthogonality. Only the front nut remains.
- A part of the axle thread has been removed, making it easier to fit the nut, and reducing the time taken to screw it on.
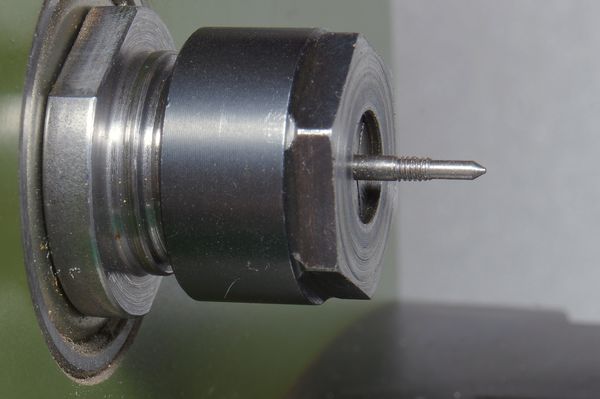
Click on the image to get a closer look at the axle.
- The carriage tool is no longer used to reduce the width, as it requires too much pressure for the width to be machined, and therefore cannot achieve the desired width in a single pass. It has now been replaced by the boring tool, which has an oblique cutting edge that allows it to cut more deeply into the material.

Click on the image to get a closer look at the tool.
All this saves a great deal of time on assembly, machining and checking dimensions.
Tyres for the Richier L’Obsidienne road roller
These tyres are made from copper plumbing tubes. Their diameter forces me to use the chuck, with its annoying runout. I explain this in detail in the article devoted to this model.
Conclusion
Working with this lathe is pleasant. It allows you to make decent parts. I certainly enjoyed using it, despite some incidents caused by my clumsiness and lack of experience. This is a real, well-finished scaled-down lathe, not a toy. There is one drawback: at high speeds, the machine is noisy, generating high-pitched whistling noises; wearing noise-cancelling headphones will not be superfluous.
What is missing is a chuck with four independently adjustable jaws. There is one with the same 16 × 1 thread, intended for the DB 250 wood lathe (Proxxon ref. 27024), but it is not adaptable to the FD 150, according to the manufacturer itself. The reason may be that its bore is not 18 mm. So, should I buy it and send it back if it does not fit? It is worth considering.
A year on…
A drawback has arisen
A rather annoying drawback has become apparent in use, concerning the carriage’s alignment mechanism. It is very difficult to adjust it so that it runs parallel to the feed axis (the graduations are wide and imprecise). This is a nuisance when you want to turn a workpiece over a long travel distance: you end up with a cone instead of a cylinder. Consequently, once adjusted, you dare not touch it again if you really need to make a cone.
Don’t touch it? Yes, but it sometimes pivots unintentionally when you loosen the toolholder! Very annoying, then.
A handy little modification
The lathe’s power cable is not very flexible. This is not a problem if you have set aside a fixed spot for the lathe, but that is not the case for me. On the contrary, the fact that this machine is compact and lightweight, making it easy to store, is a huge advantage for me. But that means the cable gets in the way quite a bit.
So I fitted the lathe with a detachable cable. Initially, I planned to install a male socket fitted into the motor housing, but there simply was not enough space. I settled for the solution of connecting a male IEC 60320 plug to the original, heavily shortened cable. I connect it to a recycled extension cable, the sort used for PC power supplies, which is much more flexible than the previous one.
A related advantage is that, when handling the machine, I can easily unplug it without having to crawl around to reach the wall power socket.

This photo highlights another drawback, though this one is less of a problem: when working close to the chuck, the travel of the cross slide is restricted by the motor cover.
FD 150/E lathe
Proxxon reéf. 24150
About €490, price 2025
at Reichelt.
Sliding tailstock chuck
Proxxon ref. 24152
About €13, price 2025
at ToolNation.
Set of ER11 collets
Proxxon ref. 24154
About €93, price 2025
at ToolNation.
Set of 6 turning tools
Proxxon ref. 24524
About €60, price 2025
at Contorion.